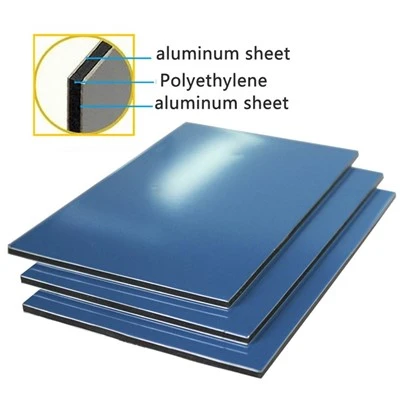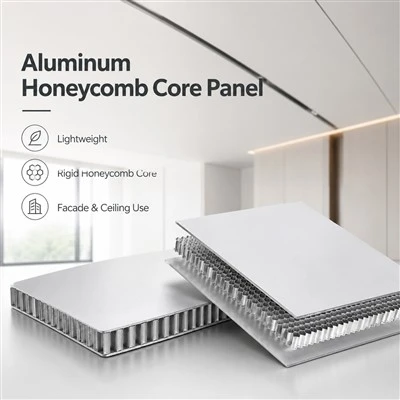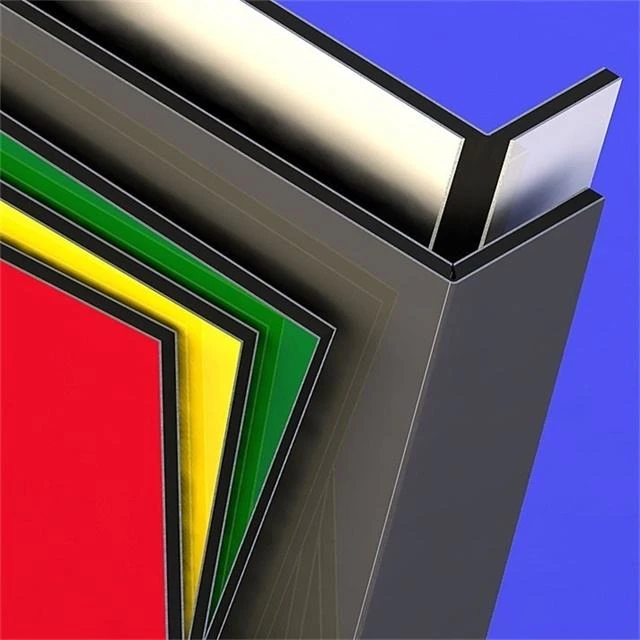
can you bend aluminum composite panel?
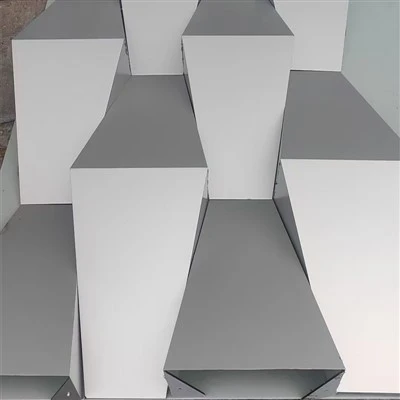
1. Sharp folds (90°, 135° returns, cassette edges) - V‑groove routing (the standard shop method)
Route a V-groove from the back side, remove most of the core, leave the front aluminium skin intact as a hinge.
Then fold cleanly by hand or light clamp pressure.
Typical inside radius after grooving: 2–3 mm.
Good for: box returns, trim, capping, sign trays, facade cassettes.
Critical rule: never cut through the front aluminium skin.
A2 mineral-core fire-rated panels are stiffer; many A2 grades are not suitable for tight V-groove folding (they crack easier).
2. Smooth curved bends (columns, rounded walls, arches) - cold roll bending, NO grooving
Use a 3-roll pyramid roller or press brake, cold form at room temperature.
Rule of thumb (PE core ACP): minimum radius ≈ 10–15 × panel thickness
3 mm panel: ~45 mm min radius
4 mm panel: ~60 mm min radius
If you force a tighter radius than this without grooving, the core cracks, the front PVDF coating crazes, or skins delaminate.
Keep protective film on during rolling to avoid scratching PVDF / FEVE finish.
There is small springback, so roll slightly tighter than target radius.
Important notes
Do not heat ACP to bend it - PE core melts, bond fails.
Anodised aluminium skins are more prone to micro-cracking along bend lines than PVDF coated.Alucobond
Double curvature (dome shapes) is possible but much harder and costly, not standard.
Always test a sample from your exact batch first; skin thickness and core type change bend behaviour.
Do you need it for sharp folded returns for your cladding cassette, or smooth curved column covers?