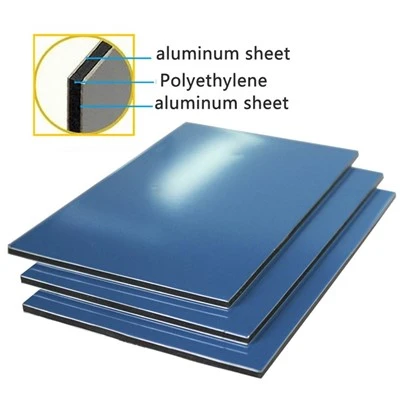
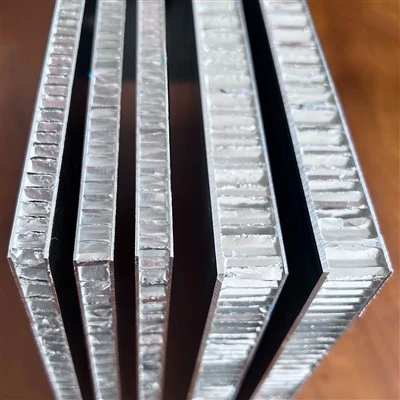
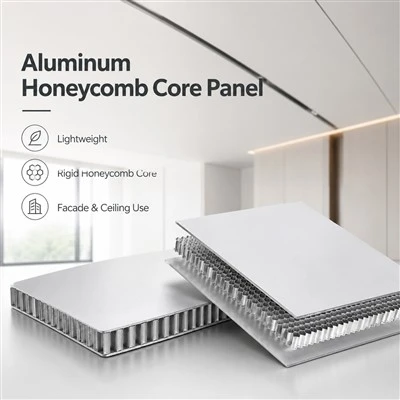
wo main ways to bend ACP / ACM (aluminum composite panel)
Important rule: Always keep the protective film on during bending to avoid scratching PVDF/polyester coating. Bend slowly; cold bending only - do NOT heat ACP to bend it.
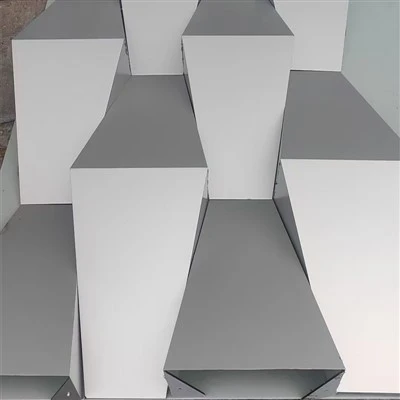
1. V‑groove routing + folding (for sharp 90°, 135° corners, cassettes, sign returns - most common for facade & sign shop)
This is how you get crisp square bends, the standard "rout & fold" method
Mark the fold line on the BACK (non‑visible side)
Use a CNC router / hand router with 90°–110° V‑groove bit
Critical depth setting: Remove core material, but leave 0.2–0.3 mm thin core layer above the front aluminum skin. ✅ Do NOT cut through the front aluminum skin - it will crack later under wind/thermal movement Example for your 1/4" (6.35 mm) ACP: groove deep enough to leave that ~0.3mm safety layer
Deburr the groove, clean dust
Bend toward the grooved side (the groove becomes the inside of the corner). Bend gradually, do not snap it.
Hold or clamp for a short time to set the angle; springback is small on routed folds.
Best for: facade cassette returns, sign letter backs, box shapes, internal corners. ❌ Not for large smooth curved surfaces.
2. Cold roll bending / press brake bending (for gentle continuous curves, columns, curved walls)
No V‑groove. You bend the whole panel as a sandwich panel.
Use 3‑roll bender, pyramid roller, or press brake with rounded soft dies
Minimum bend radius rule (PE core ACP): generally R = 10 × panel thickness
¼" (6.35 mm) ACP: safe minimum inside radius ≈ 65 mm
A2 mineral core ACP is stiffer: R = 20~25 × t, harder to bend, easier to crackalucobond....
Roll slowly, evenly; over‑bend 3–5° to compensate for springback
Rollers must be smooth, clean; use protective film between roller and panel surface
You can only make single‑axis curves (cylinders). Double curvature (bowl shape) is not practical with standard ACP.
Best for: curved column cladding, rounded building corners, curved signage faces. ❌ You cannot get a sharp 90° corner this way.
Common mistakes that ruin panels
Cut the V‑groove too deep, nick the front aluminum skin → coating cracks, delaminates outdoors
Bend the wrong direction (groove on outside) → front skin stretches and cracks
Remove protective film before bending → scratches on PVDF finish
Try to cold‑bend below the rated minimum radius
Heat the panel with torch / heat gun: PE core melts, lamination fails
Bend when temperature <15°C (59°F): coating becomes brittle, easy to craze
Quick comparison for your 1/4" (6.35 mm) ACM
| Method | Result | Min Radius | Typical use |
|---|---|---|---|
| V‑groove rout & fold | Sharp 90° corner | ~3–4 mm internal corner radius | Facade cassettes, sign boxes |
| 3‑roll cold bend | Smooth arc | ~65 mm | Curved walls, round columns |
Extra fabrication note for your ACP manufacturing business
When you supply bent ACP to clients, always state clearly:
Whether it is routed fold or cold rolled curve
Minimum bend radius
Skin thickness and coating type (PVDF is less flexible than plain polyester)
Fire grade (A2 mineral core bends much harder than PE core)