How to cut holes in ACP / ACM (aluminum composite panel)
Core rule: Keep protective film on; support the back; avoid heat - heat melts PE core and causes delamination. Four common methods, sorted from small holes to large / irregular cutouts.
1. Small round holes (drill bit, for fastener holes)
Best for screw / rivet holes, 3 mm ~ 12 mm
Mark position, use a center punch to make a tiny indent so the bit does not wander
Clamp panel down, put plywood backing under the hole (stops breakout)
Use 135° split-point HSS or carbide drill bit for aluminum
Drill at medium-low speed, light steady pressure; lift the bit often to clear chips
Deburr both sides with a deburring tool or 400–600 grit sandpaper
For exterior fixing: drill hole 2–3 mm oversized for thermal expansion (critical point you put in your installation guide) ⚠️ A2 mineral core ACP is brittle - feed even slower, easier to crack around holes.
2. Medium/large round holes (hole saw, 15 mm up to ~100 mm)
Pipes, conduit cutouts, speaker holes
Center pilot drill first, plywood back support
Use bi-metal hole saw (for non-ferrous metal), sharp teeth
Slow speed, light feed; pull out repeatedly to clear melted PE plastic
Do not force it. If smoke appears → stop, you are overheating the core
Clean melted core residue from the edge after cutting
3. Irregular / square cutouts (jigsaw)
Outlet boxes, custom shapes
Inside your marked cutout area, drill a starter hole big enough for the jigsaw blade
Keep the good finished side facing up
Use fine-tooth blade for metal / plastic
Cut slowly, steady feed; support the waste piece so it does not tear the panel at the end
File or sand rough corners
4. High-volume / clean precision (CNC router, waterjet, turret punch)
Factory production:
CNC router: single-flute up-cut bit, moderate feed + vacuum chip removal, best clean edge for batches
Waterjet: cold cut, zero heat, excellent for A2 fire-rated panels; no melting, no delamination risk
Turret punch: only good for PE core ACP; not recommended for mineral A2 core, it chips and cracks easily
Critical mistakes to avoid (very important for your customers)
Remove protective film before cutting → scratches on PVDF surface
No backing under panel → aluminum skin tears / peels on exit side
High speed + heavy pressure → heat melts PE core, delamination starts at hole edge
Using wood hole saw / dull blades → jagged edges, core stringing
Drilling too close to panel edge: minimum edge distance ≥ 2× panel thickness
Leave melted plastic stuck on hole edge: over time this traps moisture and starts delamination outdoors
Quick spec note for your TDS
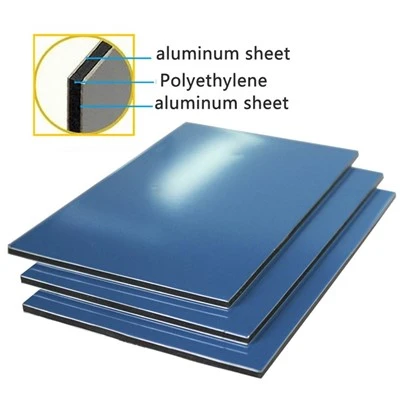
PE core ACP: forgiving, easier to drill / hole saw
B1 mineral core: slower cutting, more brittle
A2 non-combustible core: highest care, waterjet or CNC preferred over hole saw
After cutting, you can seal raw hole edges with edge sealant for exterior facade use to block water ingress
Simple comparison
| Method | Shape | Best size | Surface quality |
|---|---|---|---|
| Twist drill | Round | 3–12 mm | Good |
| Bi-metal hole saw | Round | 15–100 mm | Fair–good |
| Jigsaw | Any irregular | Medium cutouts | Fair |
| CNC / Waterjet | Any | All sizes | Excellent |
| Turret punch | Round / simple shapes | Mass production | OK only PE core |